Hygiene and Food Safety Requirements
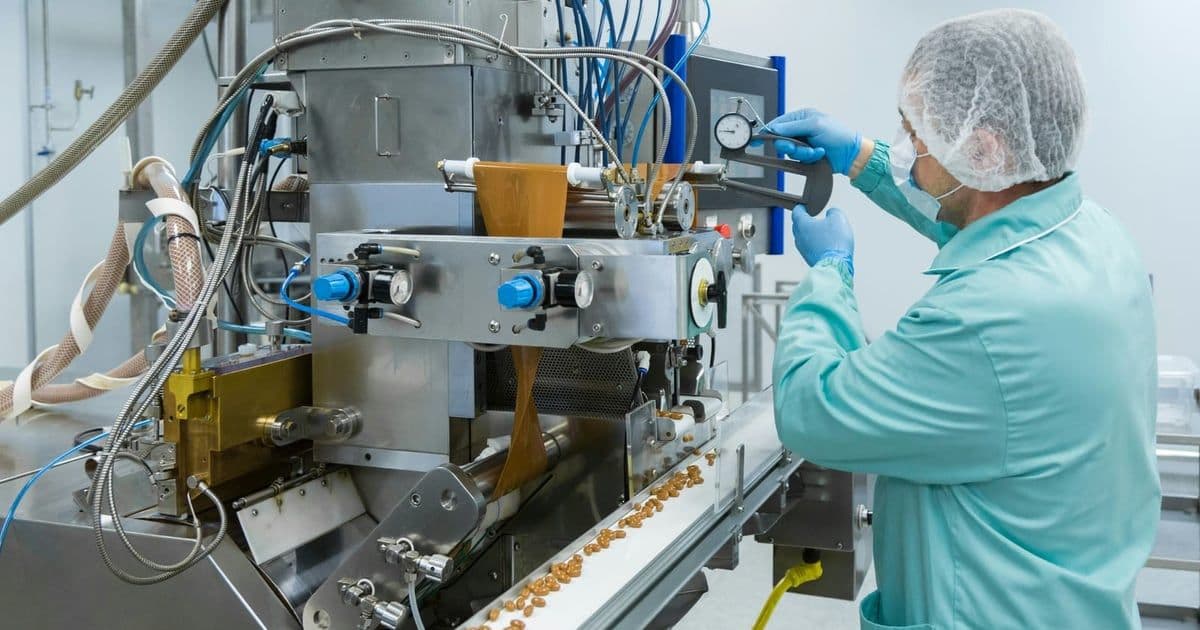
Hygiene is what sets food plant work apart. Every action is judged by its effect on food safety, from the tools brought onto the floor to the materials used in a repair.
HACCP awareness
Hazard Analysis and Critical Control Points is the food industry's safety framework. Every food plant has a HACCP plan, and anyone working in production has to know how their work touches it. That is why every tool is counted in and out, why loose items are secured, why some lubricants never go near open product. A technician who treats these as paperwork is a risk.
Hygienic design principles
Equipment in production zones is built to be cleaned. Smooth surfaces, no dead legs in the pipework, fully welded frames, sealed enclosures. A repair has to keep it that way. A rough weld, an unsealed joint or a recess you cannot clean becomes a home for bacteria. So welds are ground smooth and passivated, cable entries are sealed properly, and a temporary fix in a material you cannot clean has no place in a production zone.
Allergen management
Where a plant handles several allergens, cross-contamination control matters. That can mean changing PPE between zones, using dedicated tools and following set routes through the plant. Get it wrong and the result is a recall, regulatory action and harm to consumers.
Washdown environments
Production areas are cleaned with high-pressure water, steam and chemical sanitisers. Electrical equipment, cable management and instruments have to be rated for it, typically IP65 or higher. Every gland, enclosure seal and connector a technician disturbs has to be resealed correctly. One badly sealed cable entry lets water in. That means an electrical failure or a food safety hazard.
Common Field Service Needs
Food and beverage plants run a lot of specialised equipment. These five areas come up most.
PLC and automation
Siemens, Rockwell Automation and Schneider Electric run most European food plants. The work covers recipe management, clean-in-place (CIP) sequences, batch control, packaging line integration, checkweighers, metal detectors, vision inspection of labels and fill levels, and the traceability that ties production data to each batch.
Electrical systems
Motor control centres, drives, distribution boards and instruments, in places that are wet, cold, hot or all three. Enclosure ratings, cable management and materials have to suit the zone. Fixings are stainless, not carbon steel. Food-grade cable ties. Sealed conduit, not open tray. Production zones usually need hygiene gowning, with every tool accounted for.
Mechanical systems
Conveyors, pumps, filling machines and packaging equipment. Filler changeovers, belt replacement and tracking, pump seals and alignment, packaging machine faults. Food-grade lubricants (NSF H1 registered) are mandatory. Gaskets have to withstand the cleaning chemicals. Anything that touches product has to be food-safe.
Refrigeration and process cooling
The cold chain keeps food safe, from walk-in chillers to ammonia plants and blast freezing tunnels. Work on equipment containing fluorinated gases needs F-gas certification. Ammonia systems need competencies of their own. The temperature monitoring and alarms are critical control points.
Calibration and instrumentation
Temperature probes, pressure transmitters, flow meters and weighing systems are often HACCP critical control points, so their accuracy is a food safety matter. Calibration needs traceable certificates, documented procedures and clear pass or fail criteria. An instrument that fails is repaired or replaced before production restarts.
Certifications and Training to Consider
On top of the usual electrical and mechanical qualifications, these show a technician knows what the sector needs.
Food safety and hygiene awareness (Level 2)
Widely available, usually a day or less. Food safety principles, personal hygiene, preventing contamination. It is often the minimum for anyone entering a production area, outside technicians included.
HACCP principles training
Not always required. But a technician who knows why each control exists spots a problem before it grows.
F-gas certification
A legal requirement for work on equipment containing fluorinated gases: handling, leak checks, recovery and installation. In the EU the rules are in the F-gas Regulation (EU) 2024/573, which replaced Regulation 517/2014 in 2024. Check which certificate category the work needs.
Electrical and mechanical qualifications
The standard electrical qualifications for the country of work still apply. Mechanical technicians should hold fitting or millwright qualifications. Many manufacturers also require a site induction of several hours before any work starts, covering hygiene rules, allergen controls and emergency procedures.
Practical Tips for Hiring
Four things to put in the mission brief, so the right field service technicians apply.
Say it is a food or beverage plant
Put it in the mission brief, so technicians can judge their own experience before they apply. A brief that says only "PLC programming" draws general industrial programmers.
Say whether it is a production zone or a utility area
Production zones, where food is exposed, carry far stricter hygiene rules than plant rooms, MCC rooms or equipment outside. Say which, and the technician knows what PPE, hygiene and materials to expect.
Name the food-grade materials
Food-grade lubricants (NSF H1), stainless fittings (typically 316L), food-safe sealants and suitably IP-rated parts. A technician who turns up with standard industrial materials may not be able to finish.
Give the maintenance window
Shelf life, retail delivery slots and raw material supply set the windows. They are often shorter than in other industries because production is hard to move. Say when the window opens and closes, and what happens if the work overruns.
When you read technician profiles on FindFST, look for food and beverage experience as well as technical qualifications. A technician who lists dairy processing, bakery production or beverage bottling is more likely to know the hygiene rules than one with the same skills from general industry.
Disclaimer: This guide is general information, not professional, legal or food safety advice. Hygiene rules, certification requirements and regulations differ by country and by site, so check what applies to yours before acting on anything here. FindFST accepts no liability for decisions made on the basis of this guide.
Find Food Industry Technicians on FindFST
Post the mission with the zone, the hygiene rules and the food-grade materials the work needs, and compare the field service technicians who apply. Or search the directory by skill, industry and country.
Hire industrial field service technicians directly. No agency markup, just a flat 6% platform fee.
If you need someone for a run of shifts, shift cover fills the rota at a rate you set.